How To Make Supports Easier To Remove Cura
Okay, let's talk about one of the most satisfying moments in 3D printing. You know the one. That sweet snap when a support breaks off clean like a cold Hershey's bar. But som...
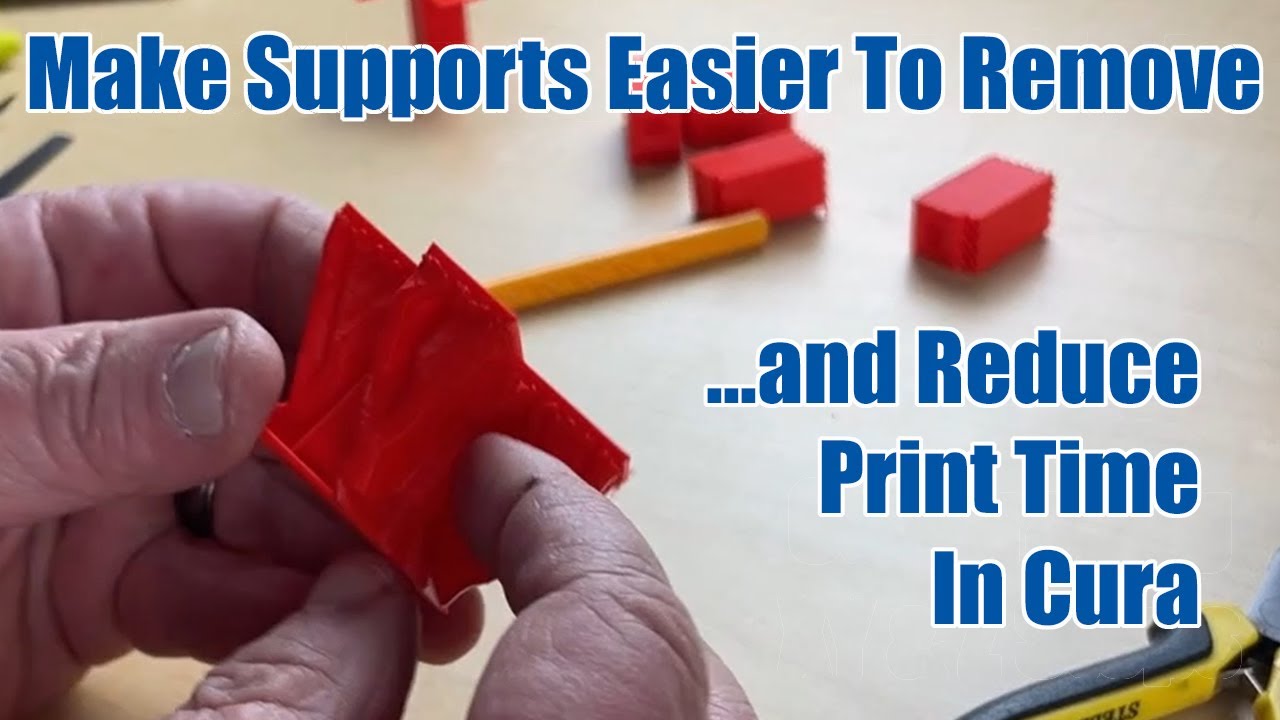
Okay, let's talk about one of the most satisfying moments in 3D printing. You know the one. That sweet snap when a support breaks off clean like a cold Hershey's bar.
But sometimes? It's more like pulling a thousand tiny teeth. Ugh.
Cura makes this way easier than you think. And honestly, this stuff is weirdly fun to mess around with.
Must Read
Start With the Right Support Structure
Cura gives you options. Obvi. You've got zigzag, grid, tree, and more. Each one behaves differently when you pull it off.
Tree supports are the crowd favorite right now. They look like weird little claymation arms reaching around your model. Creepy but awesome.
Tree supports use less material. They also hug your print like a weirdly affectionate Cthulhu. Removal feels almost effortless.
Thin Out Your Interface Layers
This is the secret sauce, my friend. Go to Support Interface in Cura's settings and set it to a thin layer count. Two or three works like a charm.
Fewer interface layers means less material glued to your model. It's simple math. Less stuff touching your print equals easier peeling.
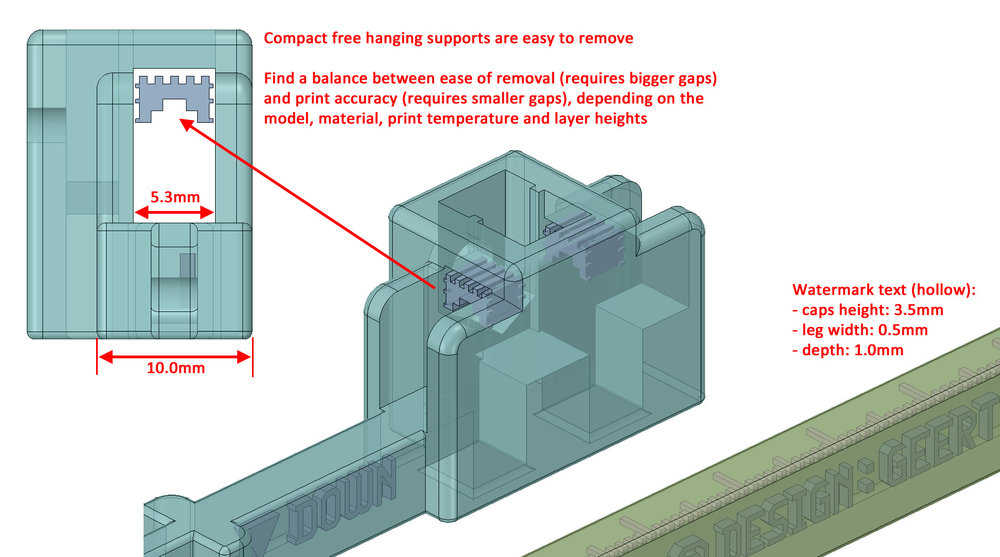 Which support patterns remove easily? - UltiMaker Cura - UltiMaker
Fun fact: this tiny tweak alone can save you hours of post-processing. That's time you could spend printing more tiny dragons. Win.
Adjust the Z Distance Between Separation
Here's another one people sleep on. Set the Z Distance between support and model higher than default. Try 0.2mm or even 0.3mm.
That little gap creates a natural air pocket. Supports detach with barely a nudge. It's like your print waves goodbye instead of clinging on for dear life.
But keep it too tight? Yeah. Say hello to the wax museum effect. Your supports fuse into your model and that's a nightmare nobody signed up for.
Fiddle With Support Density
Density controls how packed your supports are. Lower it if you don't need absolutes rock-solid support. Think 15% instead of 40%.
 Support Material: Printing and Removal - Tutorial Australia
Sparse supports snap apart easily. They're like a scaffold made of crackers instead of steel. Crunchy and quick to break.
Just don't go nuts and drop it to 5%. Your print needs some help or it turns into spaghetti before it's even spaghetti time.
Enable the Support Drop Rate
Wild as it sounds, there's a setting called Support Z-Gap or influence spread. Adjust how far the support retreats from flat surfaces.
Flat regions barely need support. Let them fly free. Save material, save time, save your sanity.
You wouldn't use scaffolding on the floor of a building, right? Same logic here. Why prop up a surface that's already sitting pretty?
 Using Supports *PROPERLY* for 3D Printing. Better success, less failure
Turn on the Right Adhesion Settings
Make sure your supports stick to the build plate and not your model face. That sounds weird but trust me. It matters.
Set Support Sync to nobody for tricky overhangs. This keeps supports off areas where they'll leave ugly marks.
Peeling support from a face is rough. It ruins the vibe. Nobody wants a 3D printed migraine serial killer. Well... maybe some of you do.
The Big Takeaway?
Cura is loaded with hidden gems just waiting for you to poke them. Ten minutes of tweaking saves you an hour of scraping.
Play with tree supports. Loosen the gaps. Drop the density. Experiment like a mad scientist with a good support system.
Snap. Peel. Done. Now go print something ridiculous and tag us with it. We'll be here waiting with a razor blade and a grin.
